English
 中文
TS‑PON Deterministic All‑Optical Network Solution for Smart Manufacturing
1. Project Overview
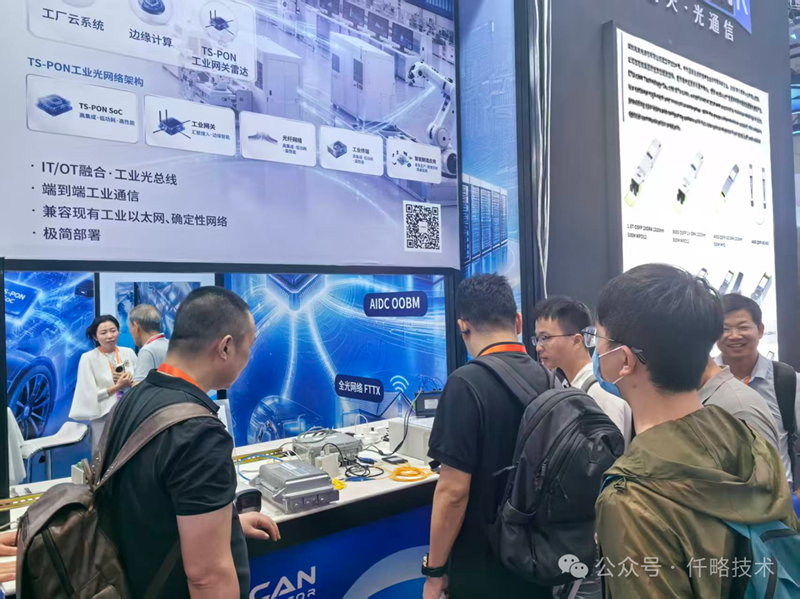
Based on TS‑PON (Time‑Sensitive Passive Optical Network) technology, this solution integrates TSN (Time‑Sensitive Networking) deterministic scheduling mechanism with the inherent advantages of passive optical networks, including long‑distance transmission, high‑bandwidth capacity, strong anti‑interference performance and simplified cabling. Targeting smart‑manufacturing scenarios such as intelligent factories, flexible production lines, industrial robot clusters, machine‑vision inspection and factory‑wide IoT deployment, it builds a deterministic all‑optical infrastructure for OT/IT convergence.
It thoroughly addresses long‑standing drawbacks of conventional industrial Ethernet, field buses and generic industrial‑PON networks, such as uncontrolled latency jitter, service contention, severe electromagnetic interference, complicated wiring, desynchronized clocks, and the inability to carry both real‑time control and high‑volume data services simultaneously. The solution achieves core networking objectives: microsecond‑level deterministic control, high‑concurrency transmission of vision‑based big data, factory‑wide device synchronization, and simple‑to‑operate‑and‑maintain networks. It supports the implementation of high‑precision manufacturing control, flexible production, AI‑powered visual inspection, digital‑twin systems and unmanned factories.
As a new‑generation industrial‑grade deterministic optical‑network technology, TS‑PON enables unified transport for real‑time OT control services and high‑volume IT data services. A single network can replace multiple heterogeneous networks including traditional EtherCAT, Profinet and common Ethernet or field‑bus systems, realizing end‑to‑end unified service delivery. It serves as an optimal transport solution for network upgrades in smart factories, retrofits of legacy production lines, and digital‑construction projects for new‑build plants.
2. Industry Status‑Quo & Construction Pain Points
2.1 Current Status of Industrial On‑Site Networks
Most manufacturing enterprises adopt a hybrid architecture of field‑bus systems plus stacked industrial switches, where control networks, vision networks, IoT networks and office networks are deployed independently. This results in fragmented protocols, multi‑tiered equipment and bloated cabling layouts. Traditional networks can only satisfy low‑speed, low‑precision and fixed‑flow production workflows, and fail to support advanced smart‑manufacturing workloads, such as multi‑robot collaboration, high‑speed servo control, 8K visual inspection, massive industrial‑sensor data collection, and real‑time digital‑twin rendering, becoming a major bottleneck hindering intelligent upgrading.
2.2 Core Operational Pain Points
Large control‑latency jitter & insufficient multi‑device coordination accuracyTraditional industrial networks deliver latency ranging from 10–50 ms with random jitter. Multi‑axis servo control, robotic‑arm collaboration and AGV formation movement suffer motion deviation and trajectory drift, failing to meet real‑time requirements for micron‑precision machining and high‑accuracy assembly.
Service contention risks with no guaranteed bandwidth for production‑critical trafficControl instructions, machine‑vision video streams, sensor readings and MES office data share network resources. During peak‑load periods, control packets may stall or drop, triggering production‑line shutdowns, higher defect rates, equipment alarms or unexpected restarts.
Poor transmission stability caused by strong on‑site electromagnetic interferenceWorkshops contain high‑density frequency converters, motors and welding equipment that generate intensive electromagnetic radiation. Conventional copper‑based Ethernet cables and field‑bus wiring are highly susceptible to interference, leading to data corruption, packet loss and intermittent link outages that disrupt continuous production.
Desynchronized device clocks prevent data correlation & traceabilityRobots, vision cameras, sensors and industrial controllers operate with unsynchronized timestamps. Inconsistent production sequencing blocks equipment interlocking, fault tracing, process review and synchronized digital‑twin modeling.
Multi‑tier equipment, complex cabling & high operation‑and‑maintenance costsMulti‑layer industrial switches, repeaters and bus nodes create numerous potential failure points. Cluttered on‑site cabling extends construction cycles, complicates troubleshooting and drives up recurring maintenance expenses.
OT‑IT network segmentation prevents converged service deliveryPhysically separated control networks and data networks use incompatible protocols, blocking integrated workflows that combine production control, data acquisition, AI analytics and platform‑level scheduling, limiting flexible‑production deployments and intelligent‑data analysis.
Restricted long‑distance workshop coverageActive‑based legacy networks feature short transmission reach and high signal attenuation, making unified networking across large‑scale campuses and multi‑workshop sites difficult.
3. Overall Solution Design
3.1 Design Principles
Deterministic‑control priority: Guarantee microsecond‑level latency, ultra‑low jitter and zero packet loss for industrial‑control traffic to meet strict closed‑loop control requirements.
Hard‑isolated multi‑service transport: Time‑slot hard‑isolation and layered priority scheduling separate control, vision, sensor‑data and MES/office traffic to eliminate bandwidth contention.
High‑reliability & EMI‑resilient design: Passive all‑optical architecture provides inherent electromagnetic‑interference immunity, adapting to harsh industrial‑workshop environments.
Unified OT/IT convergence: One single network carries both real‑time control and large‑volume data services to simplify architecture and reduce capital expenditure.
Campus‑wide high‑precision synchronization: Nanosecond‑level unified network clock to ensure accurate device coordination, fault traceability and reliable digital‑twin modeling.
Low‑maintenance operation & smooth capacity expansion: Passive nodes require zero on‑site maintenance; the network supports seamless 10G/50G bandwidth upgrades to accommodate future AI‑driven manufacturing, ultra‑high‑definition vision inspection and large‑scale IoT expansion.
3.2 Core Technical Advantages of TS‑PON for Smart‑Manufacturing Scenarios
This industrial‑grade TS‑PON (Time‑Sensitive Passive Optical Network) solution merges TSN deterministic‑scheduling technology and passive all‑optical PON architecture, delivering performance far exceeding traditional industrial‑network alternatives:
Microsecond‑level deterministic latency & jitter‑free transmissionTSN gate‑controlled time‑slot scheduling and dedicated bandwidth reservation deliver stable end‑to‑end latency ≤ 2 ms and jitter ≤ 10 μs, achieving control‑performance parity with wired field‑bus systems. This fully satisfies closed‑loop requirements for multi‑axis servo synchronization, robotic collaboration and high‑speed motion‑control workflows.
IEEE 1588v2 PTP campus‑wide clock synchronizationNanosecond‑accurate network‑wide time‑alignment synchronizes timestamps across robots, servo drives, vision cameras, sensors and industrial control systems, supporting coordinated equipment workflows, fault root‑cause analysis and real‑time digital‑twin updates.
Four‑tier hard service‑isolation mechanismTime‑slot slicing over a single optical fiber strictly separates four traffic categories: control instructions, machine‑vision streams, sensor‑acquisition data, and MES/office data. High‑priority production‑control traffic receives permanent scheduling precedence, eliminating cross‑service interference and bandwidth contention.
EMI‑resistant passive all‑optical architectureODN optical‑splitting nodes deployed on‑site are passive, unpowered and free of active failure points. Fiber‑optic transmission inherently withstands heavy workshop electromagnetic interference, removing packet loss and intermittent outages to greatly improve continuous‑production reliability.
High‑bandwidth high‑concurrency transport capabilitySymmetric 10G bidirectional transmission supports parallel delivery of multiple 8K industrial‑vision inspection streams, high‑definition workshop monitoring feeds and massive sensor‑data uploads, catering to industrial‑big‑data and AI‑vision workloads.
Long‑distance campus‑wide coveragePoint‑to‑point fiber links can span distances from 20 km to 40 km, enabling unified networking across large‑scale factory campuses and geographically separated workshops or production zones.
Simplified converged OT/IT networkingOne unified network replaces multiple heterogeneous systems, drastically reducing the quantity of switches, bus equipment and field cabling, simplifying topology and lowering construction and maintenance costs.
3.3 End‑to‑End Network Communication Architecture (TS‑PON Workshop Access + Backbone Transport)
A five‑layer deterministic networking architecture is deployed, matching the logical workflow: terminal access → workshop aggregation → campus core → application platform. TS‑PON provides deterministic last‑hundred‑meter access for industrial terminals on‑site, while the factory‑level backbone can reuse existing OTN/WDM infrastructure or industrial core‑switch hardware. This hybrid deployment forms an optimal industrial‑networking model combining deterministic edge‑access and high‑bandwidth core‑backbone transport.
Division of responsibilities: TS‑PON solves edge‑side pain points (control jitter, service contention, electromagnetic interference and clock desynchronization) at the workshop last‑hundred‑meter access layer. The factory backbone handles campus‑wide high‑bandwidth data aggregation, inter‑workshop connectivity and cloud‑platform interconnection, supporting both real‑time control and big‑data workloads.
3.3.1 Industrial Terminal Access Layer (TS‑PON Deterministic Access)
Industrial‑grade TS‑PON TSN ONUs and passive ODN optical‑splitting networks are deployed in production workshops, flexible‑manufacturing lines and intelligent workstations, connecting to a full spectrum of industrial endpoints: multi‑axis servo drives, industrial robotic arms, AGVs, 8K industrial‑vision cameras, temperature/vibration/pressure sensors, distributed PLC stations, intelligent workstation terminals and workshop‑security cameras. TSN time‑slot hard slicing isolates control, vision, sensor and data traffic classes, guaranteeing stable microsecond‑level closed‑loop‑control transmission, with all workshop‑generated traffic aggregated to the local TS‑PON OLT.
3.3.2 Workshop Aggregation Layer (TS‑PON OLT Aggregation & Scheduling)
An industrial‑grade TS‑PON OLT, located inside each workshop equipment‑room, performs terminal‑traffic aggregation, TSN time‑slot policy enforcement, priority management, local‑data buffering and traffic encryption, then forwards aggregated traffic upstream toward the campus‑core network, delivering manageable, deterministic intra‑workshop data transport.
3.3.3 Campus Core‑Backbone Layer
The factory main equipment‑room hosts industrial TSN core‑switches, TS‑PON core‑scheduling hardware, PTP precision‑clock servers, industrial‑security gateways and a plant‑wide operation‑and‑maintenance platform, interconnected to the campus backbone‑transport network. This layer manages cross‑workshop traffic scheduling, campus‑wide clock synchronization, OT/IT service convergence, security enforcement and visualized network monitoring, and establishes uplink connections to MES, SCADA, digital‑twin platforms and industrial‑cloud systems.
3.3.4 Platform Application Layer
Hosts SCADA centralized‑control systems, MES manufacturing‑execution software, AI visual‑inspection platforms, digital‑twin monitoring tools, equipment‑maintenance‑management systems and industrial‑big‑data analytics platforms, enabling end‑to‑end intelligent workflows covering production monitoring, process optimization, automated visual inspection, equipment‑fault early‑warning and full‑lifecycle production traceability.
Complete end‑to‑end communication path: Industrial production terminal → Industrial TS‑PON ONU → Passive ODN optical‑splitting network → Workshop‑side TS‑PON OLT → Factory core‑backbone network → Campus‑wide TSN scheduling platform → Industrial‑application / cloud platform
3.4 Visualized Smart‑Manufacturing Network Topology
Topology design specifications: The layered diagram clearly separates the application layer, core‑hub layer, workshop aggregation layer, passive optical‑distribution layer and end‑terminal service layer, with well‑defined boundaries between functional tiers.
4. Targeted Solutions for Key Smart‑Manufacturing Workloads
4.1 Multi‑Robot Collaboration & High‑Precision Servo Control
Scenarios: Flexible assembly production‑lines, multi‑axis linked machining, multi‑robotic‑arm coordinated workflows and AGV formation movement, requiring tightly synchronized closed‑loop‑control commands with zero motion deviation and drift, imposing strict latency, jitter and time‑synchronization requirements.
Deployment scheme: Allocate dedicated highest‑priority TSN time‑slot channels exclusively for servo‑control and robot‑motion instructions with hard bandwidth isolation. Deploy campus‑wide nanosecond‑accurate PTP clock synchronization to align motion sequences across devices. Microsecond‑level jitter eliminates motion‑coordination errors and trajectory drift, reducing defect rates and enabling micron‑precision machining and flexible collaborative production.
4.2 Real‑Time 8K AI‑Powered Industrial‑Vision Inspection
Scenarios: Surface‑defect detection, precision dimensional measurement, weld‑seam inspection and packaging‑quality verification requiring real‑time acquisition, high‑speed uplink transmission and edge‑side AI analysis of multiple 8K‑resolution image streams; high bandwidth, low packet‑loss rates and stable transmission are mandatory.
Deployment scheme: Reserve large‑bandwidth dedicated transport channels on the TS‑PON access layer for stable concurrent delivery of multiple 8K vision streams without stuttering, frame freezing or dropped frames. Vision‑inspection traffic is hard‑isolated from control‑plane traffic and never consumes production‑control bandwidth resources. This configuration enables stable parallel operation of high‑precision motion control and high‑definition visual inspection, greatly improving inspection accuracy and production throughput.
4.3 Plant‑Wide Industrial‑IoT Condition Monitoring & Fault Early‑Warning
Scenarios: Mass‑scale data collection from temperature, vibration, pressure, electric‑current and acoustic sensors deployed throughout workshops. Real‑time equipment‑health monitoring, predictive fault alerts, energy‑consumption analytics and process‑parameter traceability form foundational workloads supporting lean‑manufacturing‑oriented maintenance and cost‑reduction initiatives.
Deployment scheme: Assign dedicated transmission channels for time‑series sensor data to ensure reliable high‑volume data upload and precise timestamp alignment. The unified campus‑wide clock enables multi‑source sensor‑data correlation, traceability and historical review, supporting predictive equipment‑failure alerts, process‑parameter optimization and intelligent energy‑usage analysis.
4.4 OT/IT Convergence & Real‑Time Digital‑Twin Modeling
Traditional factory deployments maintain physically separated OT control‑networks and IT data‑networks, preventing real‑time mapping, virtual simulation and remote scheduling between physical‑plant status and digital‑twin models. Digital‑twin workloads require live synchronization of equipment states, production data and motion trajectories between physical assets and virtual replicas to achieve physical‑digital interoperation.
Deployment scheme: The unified TS‑PON infrastructure concurrently carries real‑time OT control traffic and high‑volume IT data streams. Differentiated priority scheduling guarantees deterministic control‑service performance alongside high‑concurrency big‑data transport. Plant‑wide time‑synchronization ensures perfect alignment between virtual‑twin models and physical‑production‑line states, enabling accurate digital‑twin modeling, simulation‑based deduction and remote visualized production management.
4.5 Legacy Production‑Line Network Retrofit & Simplified‑O&M Upgrade
Aging production‑line networks suffer from multi‑tiered switch hierarchies, tangled cabling, recurring failures and high maintenance overhead, with expensive downtime risks associated with retrofitting. The passive all‑optical TS‑PON architecture supports low‑impact, non‑stop‑production upgrades that drastically simplify on‑site network topologies.
Deployment scheme: Replace cascaded industrial‑switch infrastructure with passive ODN optical‑splitting nodes to eliminate multiple active failure‑points and reduce on‑site cabling volume. Industrial‑grade ONUs provide backward‑compatible interfaces to connect legacy PLC, servo‑drive and sensor hardware without large‑scale equipment replacement, delivering cost‑effective deterministic‑network upgrades for older production facilities.
5. Industrial‑Grade Technical Specifications for Core Hardware
5.1 Industrial‑Grade TS‑PON OLT
Transmission standard: 10G XG‑PON industrial specification, symmetric high‑speed uplink/downlink bandwidth
Deterministic‑performance metrics: End‑to‑end latency ≤ 2 ms; jitter ≤ 10 μs (industrial field‑bus‑equivalent control accuracy)
Clock‑synchronization: IEEE 1588v2 PTP & 1PPS precision time‑synchronization support for industrial‑process traceability
Scheduling capabilities: TSN gate‑control scheduling, four‑tier time‑slot hard‑service‑isolation, user‑configurable traffic‑priority rules
Industrial reliability: Wide‑temperature operation, dust‑and‑EMI‑resistance, link‑redundancy, link‑failure protection and hot‑standby equipment‑backup support
Supported workloads: Servo control, multi‑robot collaboration, machine‑vision inspection, industrial‑sensor data acquisition and MES office‑traffic transport
Operation‑and‑maintenance features: Plant‑wide visualized monitoring, automatic fault‑alarm generation and remote configuration & maintenance
5.2 Industrial‑Grade TS‑PON TSN ONU
Access bandwidth: Bidirectional symmetric 10G bandwidth for multi‑service deterministic delivery
Physical interfaces: Gigabit‑Ethernet ports, RS‑485 / RS‑232 serial ports for native compatibility with PLCs, servo drives, sensors and industrial‑control terminals
Deterministic capabilities: Local TSN traffic scheduling, traffic‑priority marking, time‑slot binding and expedited forwarding for closed‑loop‑control traffic
Clock‑synchronization: Built‑in PTP client for precise terminal‑level time‑alignment
Industrial‑environment resilience: Operating temperature range ‑40 °C ~ +85 °C, enhanced dust protection, electromagnetic‑interference‑resistance and vibration‑resistance, optimized for harsh‑workshop operating conditions
6. Deployment & Implementation Plan
6.1 Implementation Workflow
On‑site survey & customized solution design: Map workshop‑by‑workshop production‑line layouts, equipment inventories, service‑traffic requirements, existing cabling infrastructure and electromagnetic‑interference profiles, then create customized time‑slot‑scheduling and networking blueprints for each production zone.
Core‑equipment deployment & commissioning: Install and configure TS‑PON OLT hardware, PTP precision‑clock servers, industrial‑security gateways and the centralized operation‑and‑maintenance platform inside the main equipment‑room; configure plant‑wide clock parameters, service templates and traffic‑priority policies.
Workshop passive‑optical‑network deployment: Install passive ODN optical‑splitting infrastructure within workshops. No on‑site power supply is required for passive nodes, eliminating electrical‑installation work and active‑hardware failure‑points.
Terminal‑side hardware roll‑out: Deploy industrial TS‑PON ONUs at production‑stations and along production‑lines, establishing physical connections with robots, servo drives, vision cameras, sensors and PLC hardware to complete end‑terminal service integration.
Service tuning & policy roll‑out: Configure time‑slot hard‑isolation policies according to industrial‑traffic priority rankings, fine‑tune latency‑and‑jitter parameters for mission‑critical control services to guarantee interference‑free, stall‑free production‑traffic delivery.
Plant‑wide stress‑testing & acceptance validation: Execute comprehensive multi‑service‑concurrency, maximum‑bandwidth, fault‑switchover, time‑synchronization and anti‑interference validation testing to verify stable production‑line operation.
O&M‑staff training & project hand‑over: Deliver specialized technical‑training sessions covering equipment maintenance, policy‑configuration workflows and fault‑troubleshooting procedures for on‑site engineering teams, and transfer the complete set of project‑related technical documentation.
6.2 Key Deployment‑Project Advantages
Non‑stop‑production retrofits with minimal operational disruption: Zone‑based staggered‑construction schedules eliminate mandatory full‑plant shutdowns, preserving continuous manufacturing workflows.
Simplified cabling and cost‑reduction: Passive‑optical infrastructure replaces multi‑tier switch deployments, cutting hardware‑procurement, cabling and recurring maintenance expenses.
Full backward compatibility: Interoperates with pre‑existing industrial hardware, industrial‑control systems and MES platforms without costly mass equipment‑replacement.
Future‑proof scalable architecture: Supports straightforward bandwidth upgrades, workstation expansion and new‑service integration to accommodate long‑term smart‑manufacturing evolution.
7. Industrial‑Network‑Security & Compliance Framework
7.1 Dual‑Layer Traffic‑Isolation Security Architecture
A two‑tier security‑protection model is implemented: logical time‑slot hard‑isolation at the TS‑PON access layer plus dedicated service‑channel isolation at the network‑core layer. Production‑control traffic is completely segregated from office and large‑volume data traffic, preventing unauthorized cross‑domain access, service interference and lateral malware propagation, providing foundational cybersecurity safeguards for industrial production networks.
7.2 Multi‑Layer Industrial‑Cybersecurity Defenses
Terminal whitelist admission control: Every industrial ONU and production‑site endpoint must complete identity‑verification before joining the production network, blocking access by unauthorized devices.
End‑to‑end service‑data encryption: Production‑control instructions, process parameters and equipment‑operation logs are encrypted during transmission to defend against data tampering and eavesdropping.
Plant‑wide traffic auditing: Real‑time network‑flow monitoring and permanent log‑storage support anomaly‑alerting, fault‑root‑cause tracing and regulatory‑compliance audits.
Industrial‑attack mitigation protection: Defend against DoS attacks, port‑scanning activities and malformed‑packet flooding, preventing network‑security incidents that trigger production‑line outages.
7.3 Industry Regulatory‑Standard Compliance
The solution fully complies with the Guidelines on Information‑Security Protection for Industrial‑Control Systems, Class‑2 Cybersecurity Protection Standard and national smart‑manufacturing network‑security specifications, meeting requirements for high‑reliability, robust security and full traceability within industrial‑control networks.
8. Intelligent Operation‑and‑Maintenance Support System
8.1 Visualized Smart‑O&M Platform
A plant‑wide industrial‑optical‑network management system delivers visualized monitoring of equipment online‑status, optical‑link loss, service‑traffic throughput, latency‑jitter metrics and terminal‑access conditions. It automatically identifies link anomalies, hardware failures and service‑performance degradation, enabling sub‑second fault‑alerting and fast root‑cause localization to drastically improve maintenance‑team efficiency.
8.2 Link & Hardware Redundancy Protection
Core‑network hardware and primary fiber‑optic links support hot‑standby redundancy and automatic fault‑switchover, ensuring production‑critical services remain unaffected during sudden equipment‑or‑link failures. Passive ODN optical‑distribution segments contain zero active failure‑points, delivering superior long‑term operational stability compared with conventional switch‑based workshop networks and supporting 7 × 24‑hour uninterrupted production.
8.3 After‑Sales Maintenance & Service Framework
7 × 24‑hour technical support is available, with a dedicated industrial‑network rapid‑response team for troubleshooting and service‑policy optimization. Scheduled on‑site campus inspections, parameter fine‑tuning and hardware‑maintenance activities are conducted periodically, ensuring sustained long‑term network performance supporting smart‑manufacturing workflows.
9. Solution‑Delivered Value & Benefit Analysis
9.1 Production‑Performance Benefits
Eliminates legacy‑network pain‑points such as excessive jitter, electromagnetic interference and device‑synchronization errors, improving multi‑equipment coordination accuracy, finished‑product yield‑rates and reducing manufacturing waste. Enables deployment of advanced smart‑manufacturing workloads including flexible‑production workflows, multi‑robot fleets, AI visual‑inspection and digital‑twin systems, lifting overall factory‑intelligence levels and production throughput. Unified plant‑wide timestamps and traceable datasets facilitate process‑optimization work‑flows, post‑incident production‑fault reviews and lean‑manufacturing management initiatives.
9.2 Operation‑and‑Maintenance Cost Benefits
Passive all‑optical network architecture drastically reduces the total quantity of active network hardware, failure‑points, power‑consumption requirements and field‑cabling expenditure, lowering capital‑construction costs. Simplified network topology paired with intelligent centralized monitoring reduces manual troubleshooting overhead, recurring maintenance expenses and production‑downtime durations triggered by network failures.
9.3 Digital‑Transformation Strategic Benefits
Builds a deterministic all‑optical foundational infrastructure for smart‑manufacturing, delivering end‑to‑end OT/IT network convergence and creating unified data pipelines spanning equipment control, sensor‑data collection, AI‑driven analytics and cloud‑platform scheduling. It provides core network support for unmanned, flexible and fully‑digitalized factory upgrades and future‑proofs the facility for emerging workloads including industrial‑AI, 5G‑industrial connectivity and campus‑wide IoT deployments.
10. Project‑Risk Assessment & Mitigation Strategies
Risk: Legacy‑equipment protocol‑incompatibility with TSN scheduling Mitigation: Deploy dedicated interface‑adaptation modules and protocol‑conversion hardware to reuse pre‑existing on‑site equipment, avoiding costly full‑scale production‑line hardware‑replacement.
Risk: Production‑downtime caused by on‑site construction‑related activities Mitigation: Adopt zone‑by‑zone, staggered‑hour construction‑schedules and progressive segment‑by‑segment service cut‑over workflows, maintaining continuous manufacturing‑operation.
Risk: Maintenance‑team skill‑gaps for TS‑PON new‑technology operation Mitigation: Deliver dedicated technical‑training workshops, comprehensive printed operation‑and‑maintenance manuals and permanent remote‑technical‑support channels to provide ongoing long‑term technology‑assistance.
Risk: Temporary‑service‑fluctuations during migration from legacy networks to TS‑PON infrastructure Mitigation: Run old and new networks in parallel during the transitional cut‑over phase, gradually migrating workloads while continuously monitoring service‑health metrics to achieve seamless, low‑risk network‑migration.
11. Conclusion & Outlook
This TS‑PON deterministic all‑optical‑network solution for smart‑manufacturing innovatively combines TSN time‑sensitive deterministic‑scheduling technology and passive all‑optical PON architecture. It resolves core limitations found within traditional industrial‑networks: severe electromagnetic interference, uncontrolled latency‑jitter, inter‑service bandwidth contention, desynchronized equipment clocks, bloated multi‑tier topologies and OT‑IT network segmentation. It delivers microsecond‑low‑latency, jitter‑free, EMI‑resistant, hard‑isolated and fully‑traceable deterministic‑network transport for mission‑critical smart‑manufacturing workloads: high‑precision servo‑control, multi‑robot collaboration, AI‑powered visual‑inspection, campus‑wide IoT sensing and digital‑twin systems. Featuring simplified network‑architecture, cybersecurity‑compliant operation, low‑maintenance characteristics and proven resilience under harsh industrial‑workshop operating‑conditions, the TS‑PON solution is widely applicable for new‑build precision‑manufacturing facilities, flexible‑production‑line deployments, intelligent factories and unmanned‑plant construction or legacy‑site‑retrofit projects.
TAG: